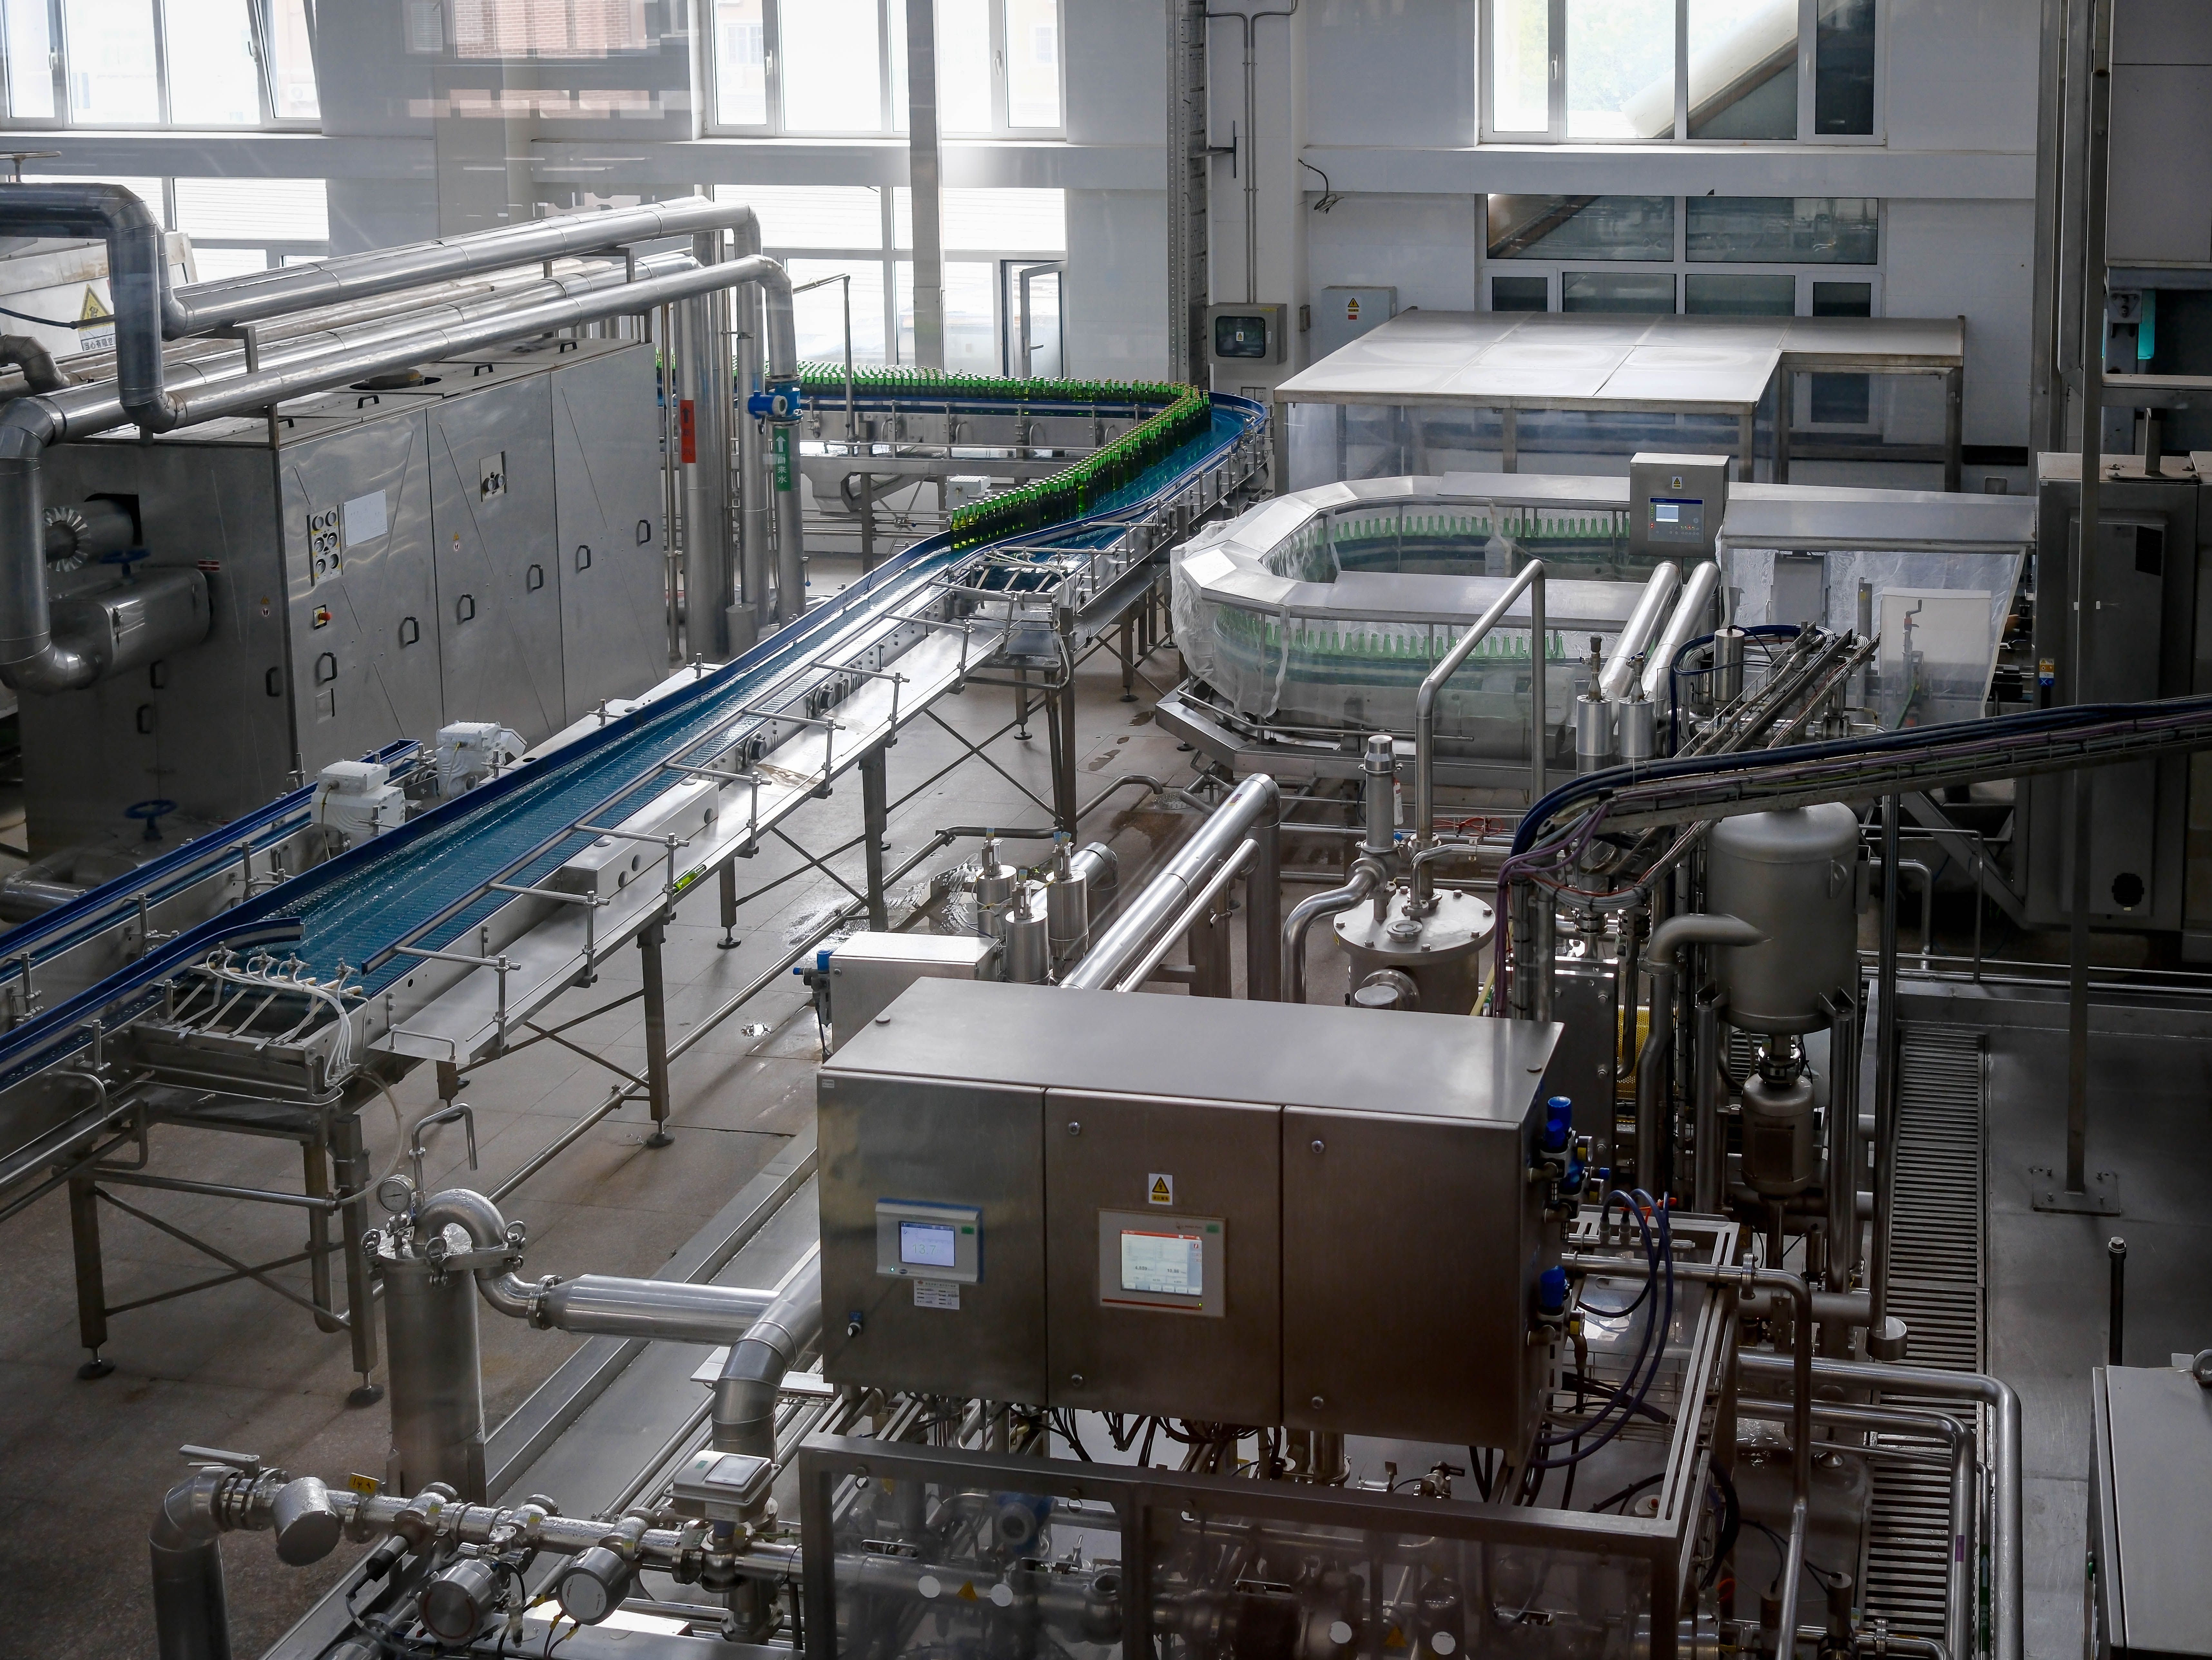
A food processing company needed a new automated conveyor line for a 50,000-square-foot facility producing more than 279,000 pounds of chocolate every two weeks. The line had to accommodate different products while maintaining consistent temperature and speed control.
The customer also needed temperature monitoring across kitchen equipment and bulk storage tanks. Staying within budget and achieving a fast startup were priorities, with the opportunity to test the complete line and make adjustments before installation.
Premier Automation designed, built, and installed an automated conveyor line using PLCs, HMIs, and drives. The system included temperature readouts for kitchen equipment and bulk storage tanks, giving operators visibility into conditions throughout the process.
A custom HMI allowed operators to adjust temperature and conveyor speed for different chocolate products on the same equipment. Premier assembled, wired, and ran the complete line in-house before installation, allowing the customer to review its operation and request changes before startup.
The automated line helped the customer bring its new facility into operation and increase capacity to meet growing demand. A packing process that previously required eight workers could now run with four, at twice the speed.
Operators also gained adjustable production settings and temperature visibility across key equipment. In-house testing helped reduce startup time, and the customer planned to work with Premier Automation on additional conveyor lines as the business expanded.
Whether you're planning a modernization project or facing a system issue that needs answers now, Premier Automation is ready to help. Tell us what you're working with, and our engineering team will bring the expertise to move you forward.